For those in the agricultural and fertilizer processing industries, understanding the functionality and advantages of modern fertilizer pneumatic conveying systems is crucial. These systems are essential for efficiently transporting bulk materials like fertilizers from one location to another, ensuring smooth operations in production and distribution. This article will delve into the working principle and key features of such equipment, highlighting how they enhance operational efficiency and reliability.
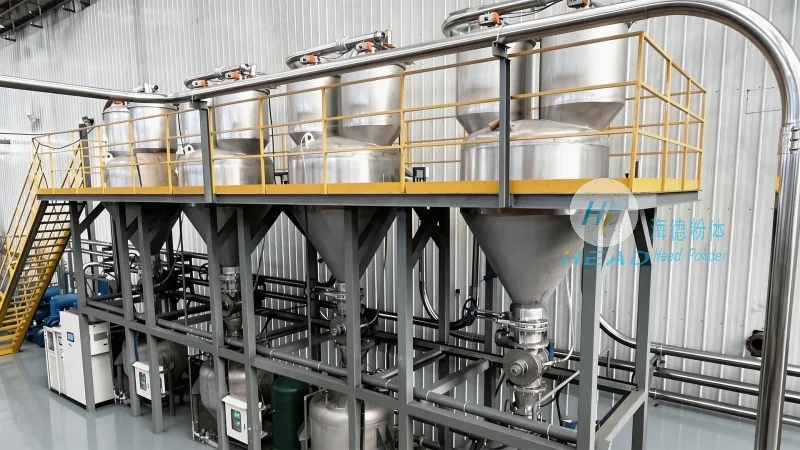
The core of a fertilizer pneumatic conveying system lies in its ability to use air to move bulk materials. The system typically operates on one of two main principles: suction (or negative pressure) or pressure (or positive pressure) systems. In a suction system, a vacuum is created at the material inlet, drawing the fertilizer into the system and transporting it through a network of pipes to the discharge point. Conversely, a pressure system uses compressed air to push the material through the pipes. Both methods rely on a combination of components that work in tandem to ensure effective material transfer.
Key components of a typical fertilizer pneumatic conveying system include the material feeder, which introduces the fertilizer into the system; the air supply unit, which provides the necessary air pressure or vacuum; the conveying line, which is the main pipeline transporting the material; the separation and cleaning equipment, which separates the material from the air and cleans the system; and the discharge device, which releases the fertilizer at the destination. Each component plays a critical role in the overall operation, and their design and integration directly impact the system's performance.
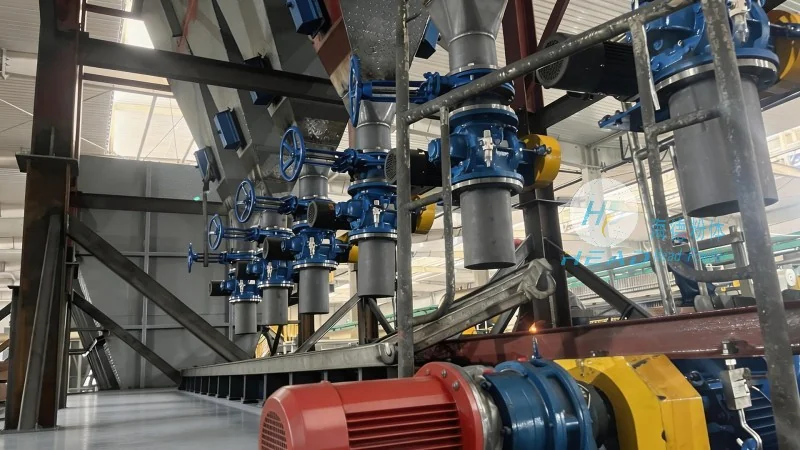
Modern fertilizer pneumatic conveying systems offer several distinct advantages that make them a preferred choice in many industrial applications. One of the primary features is their high efficiency in material handling. By using air to transport bulk materials, these systems can move large quantities of fertilizer quickly and with minimal labor, reducing downtime and increasing production throughput. This efficiency is particularly beneficial in large-scale fertilizer production and distribution centers where speed and volume are critical.
Another notable feature is the system's ability to handle a wide range of fertilizer types and particle sizes. Whether dealing with granular, powdered, or even bulk solid fertilizers, pneumatic conveying systems can adapt to different material characteristics. This versatility is achieved through adjustable air flow rates and appropriate feeder designs, ensuring that the material is conveyed without clogging or degradation. The system's design also allows for easy integration with existing production lines, making it a flexible solution for various industrial setups.
Furthermore, pneumatic conveying systems are known for their hygienic and dust-free operation. Unlike traditional belt or bucket elevators, these systems minimize dust generation and contamination, which is essential for maintaining product quality and compliance with environmental regulations. The enclosed pipeline system also helps in controlling dust emissions, contributing to a safer working environment. This feature is especially important in industries where product purity and safety are paramount.
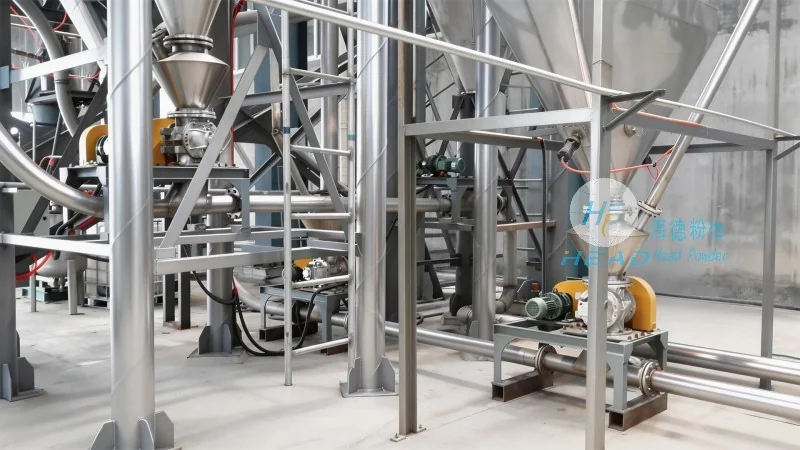
Reliability and low maintenance are additional key features of fertilizer pneumatic conveying systems. The mechanical components, such as the feeder and air compressor, are designed for durability and long service life. Regular maintenance, including cleaning and checking air pressure, is straightforward and can be performed by trained personnel. This reduces the need for frequent repairs and extends the system's operational lifespan. The system's simplicity in design also contributes to its reliability, as fewer moving parts mean fewer points of failure.
Fertilizer pneumatic conveying systems are sophisticated pieces of equipment that combine advanced engineering with practical functionality to meet the demands of modern fertilizer processing and distribution. By understanding their working principles and features, businesses can make informed decisions about implementing such systems to enhance their operational efficiency and product quality. For those seeking reliable and efficient solutions, Shandong HeadPowder Engineering Co., Ltd. offers high-quality pneumatic conveying systems tailored to meet specific industry needs. With a focus on precision and durability, HeadPowder provides equipment that ensures smooth and effective material handling, supporting the success of agricultural and fertilizer operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top