

[AIR-PNEUMATIC CONVEYING IN THE BULK HANDLING OF MOIST SODIUM NITRATE]
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field of bulk material handling, specializes in advanced air-pneumatic conveying systems tailored for the transportation of moisture-containing sodium nitrate. With a strong presence in China, particularly in Shandong province, the company leverages cutting-edge technology to address the unique challenges associated with handling this specific chemical compound. This article explores the application of air-pneumatic conveying in the efficient and reliable bulk transport of moist sodium nitrate, highlighting the technical advantages and practical implementations offered by HeadPowder's engineering solutions.
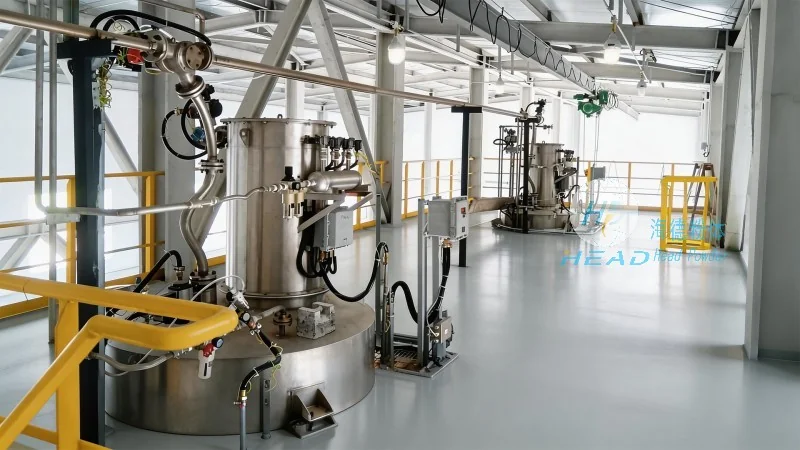
The Challenges of Handling Moist Sodium Nitrate
Moist sodium nitrate, a common industrial chemical used in fertilizers, explosives, and other applications, presents distinct handling challenges due to its hygroscopic nature and potential for caking or agglomeration when exposed to moisture. Traditional bulk handling methods, such as belt conveyors or mechanical screw conveyors, may struggle with maintaining product integrity and preventing material degradation during transport. The presence of moisture can lead to increased friction, reduced flowability, and even blockages in conventional systems, necessitating specialized equipment designed to accommodate these characteristics. Air-pneumatic conveying offers a solution by utilizing a stream of air to transport the material in a fluidized or suspended state, minimizing direct contact with equipment surfaces and reducing the risk of caking or degradation.
Advantages of Air-Pneumatic Conveying for Moist Sodium Nitrate
HeadPowder's air-pneumatic conveying systems are engineered to deliver superior performance in the handling of moist sodium nitrate. The primary advantage is the ability to maintain product quality by reducing exposure to mechanical stress and moisture. Unlike mechanical conveyors that rely on physical contact, pneumatic systems use air to move the material, ensuring minimal friction and preventing the formation of clumps. This results in a more consistent flow rate and reduced risk of material degradation, which is critical for applications where the chemical properties of sodium nitrate must be preserved. Additionally, air-pneumatic conveying allows for flexible system designs, enabling vertical, horizontal, or inclined transport without the need for complex machinery or extensive infrastructure modifications. The system's adaptability makes it suitable for various industrial settings, from small-scale processing plants to large-scale bulk handling facilities.
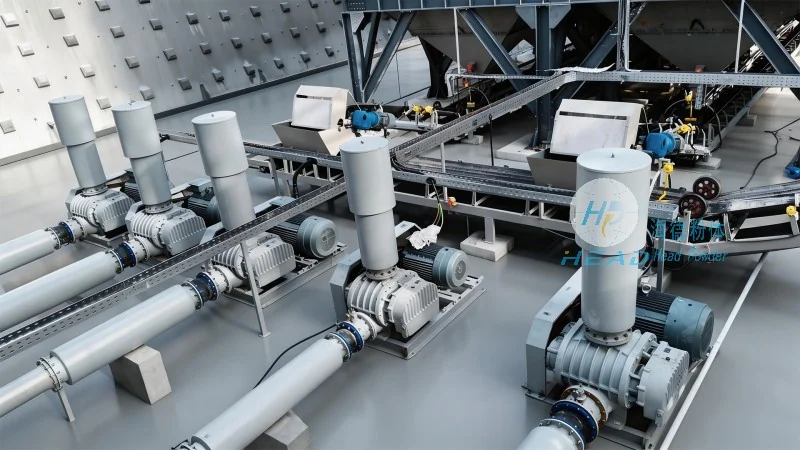
Technical Design and Implementation
HeadPowder's air-pneumatic conveying solutions are customized to meet the specific requirements of each client, considering factors such as material flow rate, distance, and environmental conditions. The systems typically consist of a series of components, including a hopper for material storage, a rotary airlock to control material feed, a conveying pipeline, and a receiver for material discharge. The use of positive or negative pressure systems depends on the application, with positive pressure being common for transporting moist sodium nitrate to prevent moisture absorption from the environment. The pipeline design incorporates smooth, corrosion-resistant materials to avoid material buildup and ensure long-term durability. HeadPowder employs advanced control systems to monitor and regulate the conveying process, ensuring consistent performance and minimizing downtime. This integration of technology allows for real-time adjustments to flow rates and pressure, optimizing the system's efficiency and reliability.
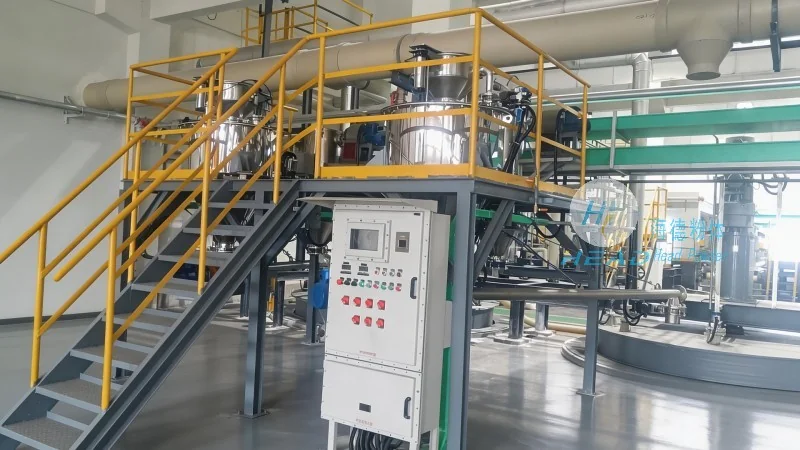
Real-World Applications and Performance
The effectiveness of air-pneumatic conveying in handling moist sodium nitrate has been demonstrated in various industrial applications. For example, in fertilizer production facilities, the system ensures that sodium nitrate is transported from storage silos to processing units without loss of moisture or quality. In explosives manufacturing, where precise control over material characteristics is essential, the conveying system maintains the chemical integrity of the product, preventing any changes that could affect its performance. The consistent flow and low degradation rates achieved by HeadPowder's systems have led to improved operational efficiency and reduced maintenance costs for clients. Additionally, the flexibility of the system allows for easy integration with existing infrastructure, minimizing the need for major renovations or downtime during installation. This adaptability has made air-pneumatic conveying a preferred choice for industries seeking reliable and efficient bulk handling solutions for moisture-containing materials.
Conclusion and Company Commitment
Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative and reliable air-pneumatic conveying solutions for the bulk handling of moist sodium nitrate. By leveraging advanced engineering and technology, the company ensures that its systems meet the highest standards of performance, safety, and efficiency. With a strong presence in China and a focus on customer satisfaction, HeadPowder continues to be a trusted partner for industries requiring specialized bulk material handling solutions. The application of air-pneumatic conveying not only addresses the unique challenges of handling moist sodium nitrate but also contributes to overall operational excellence, making it an essential component in modern industrial processes.