

Operation Process and Working Principle of Wheat Material Handling Systems
Wheat material handling systems are essential for efficient agricultural and industrial operations, ensuring the smooth transport of wheat from storage to processing facilities. These systems integrate advanced engineering and technology to optimize the flow of grain, enhancing productivity and reducing operational costs. Understanding the operation process and working principles of such systems is crucial for stakeholders in the agricultural and food processing industries.
Key Components and Their Roles
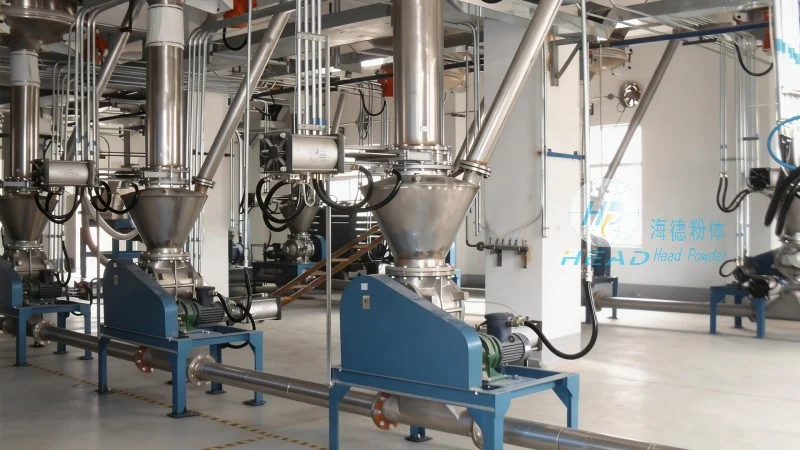
The wheat material handling system typically consists of several key components, each playing a vital role in the overall operation. These components include feeders, conveyors, elevators, and storage bins. Feeders are responsible for controlling the flow of wheat from storage silos or trucks, ensuring a consistent and controlled feed rate. Conveyors, such as belt conveyors or chain conveyors, transport the wheat horizontally or at an incline, while elevators, like bucket elevators or screw conveyors, lift the grain vertically to higher levels for processing or storage. Storage bins are used to temporarily hold the wheat, providing a buffer between the handling system and downstream processes.
The Operation Process: From Harvest to Processing
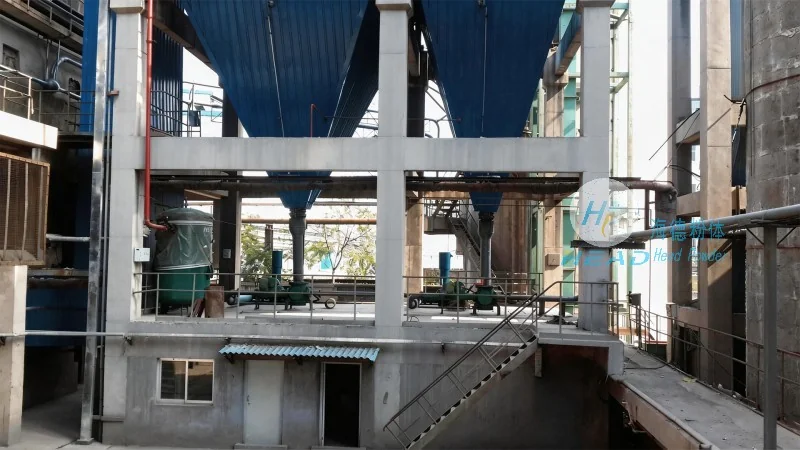
The operation process of a wheat material handling system begins with the reception of harvested wheat. The grain is first delivered to the receiving area, where it is unloaded from trucks or other transport vehicles. The feeders then take over, regulating the flow of wheat into the conveyor system. The conveyors transport the wheat to the elevators, which lift it to the desired height. The grain is then transferred to the storage bins, where it is held until it is needed for processing. When processing begins, the wheat is drawn from the storage bins and fed back into the conveyor system, moving it through the processing stages, such as cleaning, drying, and milling. The system ensures that the wheat moves efficiently and safely through each stage, minimizing loss and maximizing throughput.
Working Principles: Mechanical and Electrical Systems
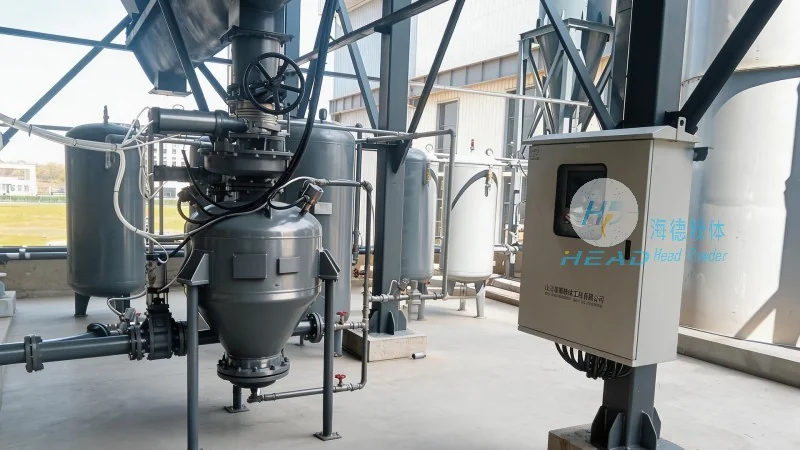
The working principles of a wheat material handling system rely on a combination of mechanical and electrical components. The mechanical parts, including conveyors, elevators, and feeders, are designed to handle the physical movement of the wheat. These components use various mechanisms, such as belts, chains, buckets, and screws, to transport the grain. The electrical systems control the operation of these mechanical parts, regulating speed, direction, and flow rates. Sensors and control panels monitor the system's performance, ensuring that it operates within safe and efficient parameters. For example, level sensors in the storage bins detect when the bin is full or empty, triggering the feeder to adjust its output accordingly. This integration of mechanical and electrical systems allows for precise control and automation, enhancing the system's reliability and performance.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of wheat material handling systems. With a focus on innovation and quality, the company has developed advanced solutions to meet the diverse needs of the agricultural and food processing industries. HeadPowder's systems are designed to be durable, efficient, and cost-effective, providing customers with reliable equipment for their wheat handling operations. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner in the industry, serving clients both domestically and internationally.
Conclusion: Enhancing Efficiency in Wheat Handling
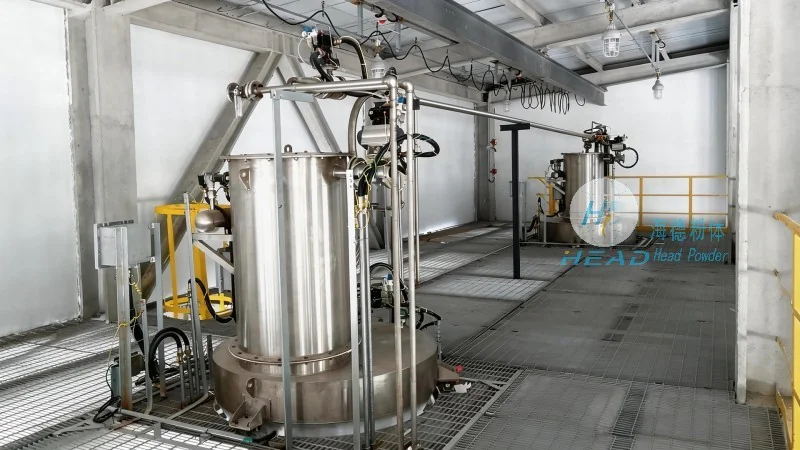
In conclusion, wheat material handling systems are critical for optimizing the flow of wheat from harvest to processing. The operation process and working principles of these systems involve a coordinated effort of mechanical and electrical components, working together to ensure efficient and safe transport. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced solutions that enhance productivity and reduce operational costs. By understanding and implementing these systems, agricultural and food processing businesses can improve their overall efficiency and competitiveness in the market.