For industrial applications involving the handling of corn starch, the selection of an efficient and reliable conveying system is crucial. Among the various options available, the corn starch pneumatic conveying system stands out as a preferred solution due to its ability to transport bulk materials like corn starch with minimal contamination and high operational efficiency. This article delves into the working principle and key features of such systems, providing insights into how they operate and why they are widely adopted in the industry.
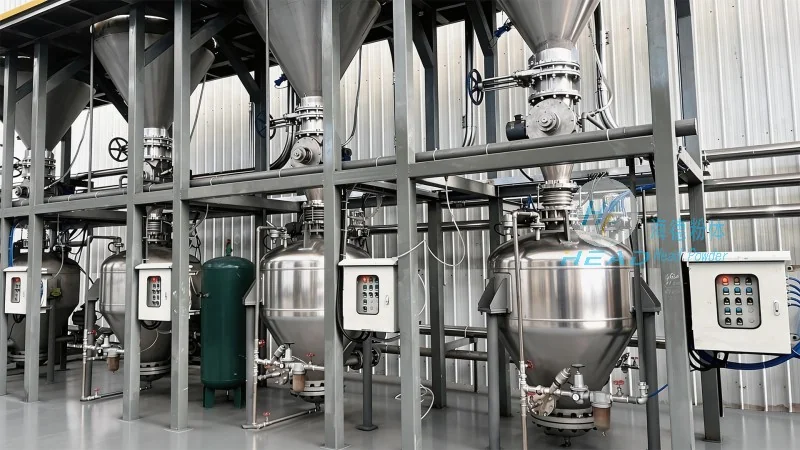
The core of a corn starch pneumatic conveying system lies in its use of air as the medium to transport the material. The system operates by creating a pressure differential or vacuum to move the corn starch particles through a pipeline. There are primarily two types of pneumatic conveying systems: pressure and vacuum systems. In a pressure system, compressed air is introduced into the conveying line at the inlet, where the corn starch is fed. The air then propels the material forward, ensuring a continuous flow. Conversely, a vacuum system draws the material into the pipeline using a vacuum pump at the discharge end, creating a suction effect that pulls the corn starch through the system. Both methods are designed to handle fine powders like corn starch effectively, preventing clogging and ensuring consistent material transfer.
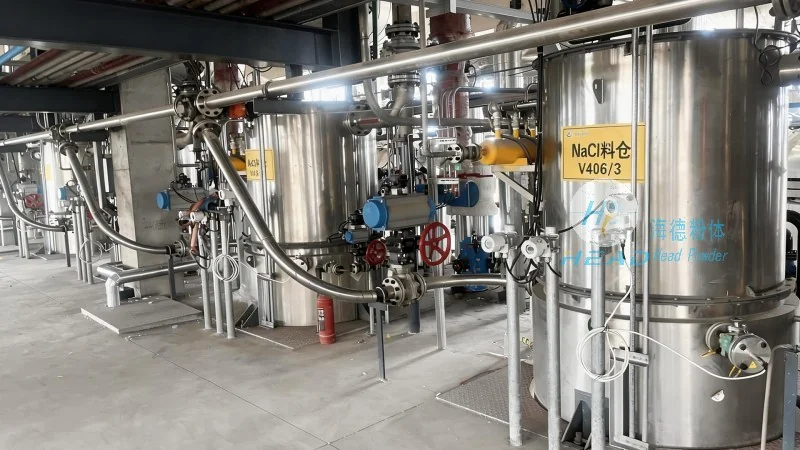
Several distinctive features make corn starch pneumatic conveying systems ideal for industrial use. Firstly, these systems offer excellent dust control, which is critical when handling fine powders such as corn starch. The enclosed pipeline design minimizes dust dispersion, contributing to a cleaner working environment and reduced health risks for operators. Secondly, the systems provide high conveying efficiency, capable of transporting large volumes of corn starch over considerable distances with minimal energy consumption. This efficiency is achieved through optimized air flow rates and pipeline design, ensuring that the material moves smoothly without excessive pressure drops. Thirdly, the equipment is designed for easy maintenance and cleaning. The modular construction allows for quick disassembly and cleaning of the conveying lines, which is essential for maintaining hygiene standards, especially in food processing applications where corn starch is used. Additionally, the systems are highly adaptable, capable of handling different particle sizes and moisture contents of corn starch, making them versatile for various industrial processes.
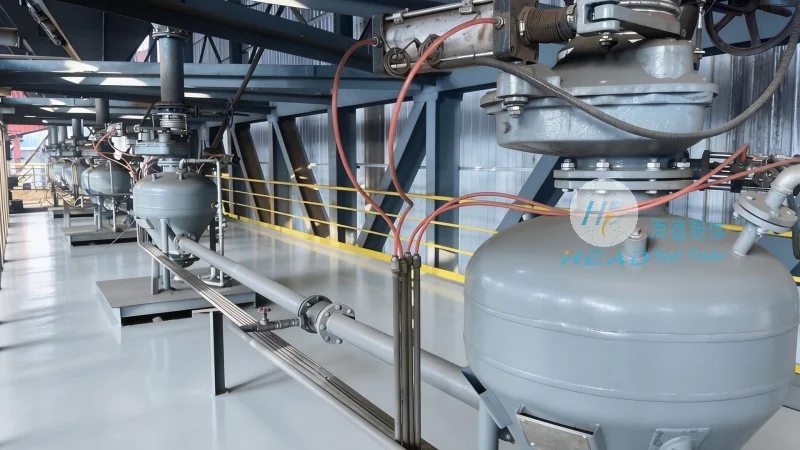
The advantages of corn starch pneumatic conveying systems are evident in their application across various industries. In the food and beverage sector, these systems are used for transporting corn starch in flour mills, starch processing plants, and food manufacturing facilities. The hygienic design and dust control features align with food safety regulations, ensuring that the product remains uncontaminated throughout the conveying process. In the chemical and pharmaceutical industries, the systems are employed for handling corn starch as an ingredient in formulations, where precision and cleanliness are paramount. The ability to maintain low contamination levels and control particle size distribution is particularly beneficial in these sectors. Furthermore, the systems contribute to operational cost savings by reducing labor and equipment downtime. The efficient material transfer minimizes the need for manual handling, which not only improves safety but also enhances overall productivity. The reliability of the system, with its low maintenance requirements, ensures consistent performance over extended periods, providing a stable and cost-effective solution for businesses.
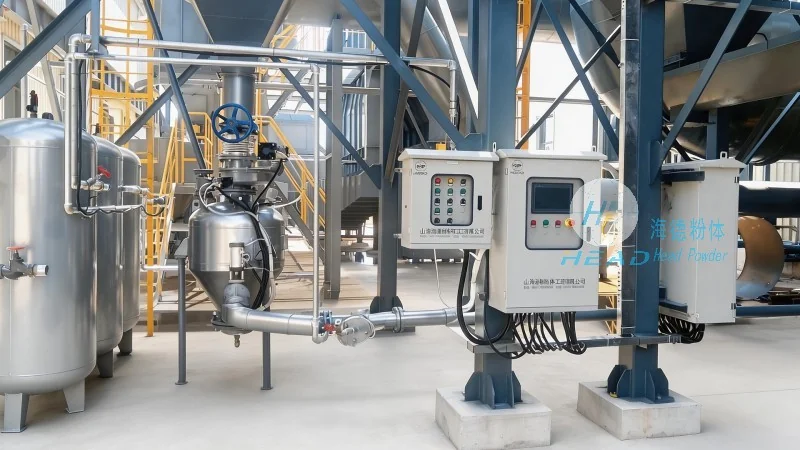
In conclusion, the corn starch pneumatic conveying system is a sophisticated and efficient solution for transporting bulk materials like corn starch. Its working principle, based on air movement through a pressure or vacuum system, ensures reliable and clean material transfer. The key features, including excellent dust control, high efficiency, easy maintenance, and adaptability, make it a preferred choice in various industrial applications. For businesses seeking to optimize their material handling processes, investing in a well-designed pneumatic conveying system can lead to significant improvements in productivity and operational safety. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and manufacturing high-quality corn starch pneumatic conveying systems tailored to meet the specific needs of different industries. With a focus on innovation and customer satisfaction, the company ensures that its systems are built to the highest standards, providing reliable and efficient solutions for material handling challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top